Machining, welding, cutting, forming, finishing, and design help, all in one 28,000 square foot building in Louisburg, NC. Bring a print or a sketch.
Bring a concept, a rough sketch, a problem, or a finished print. CAD modeling, material selection, and design for manufacturability come from the same people who build the part. Both owners are engineers, one in welding and one in electrical and mechanical systems, and both have taken hardware from concept through commissioning.
A design review is included with every parts order, no separate fee. Larger engineering work, like a new machine or a ground up product, gets a scoped design phase up front that is credited toward the production order.
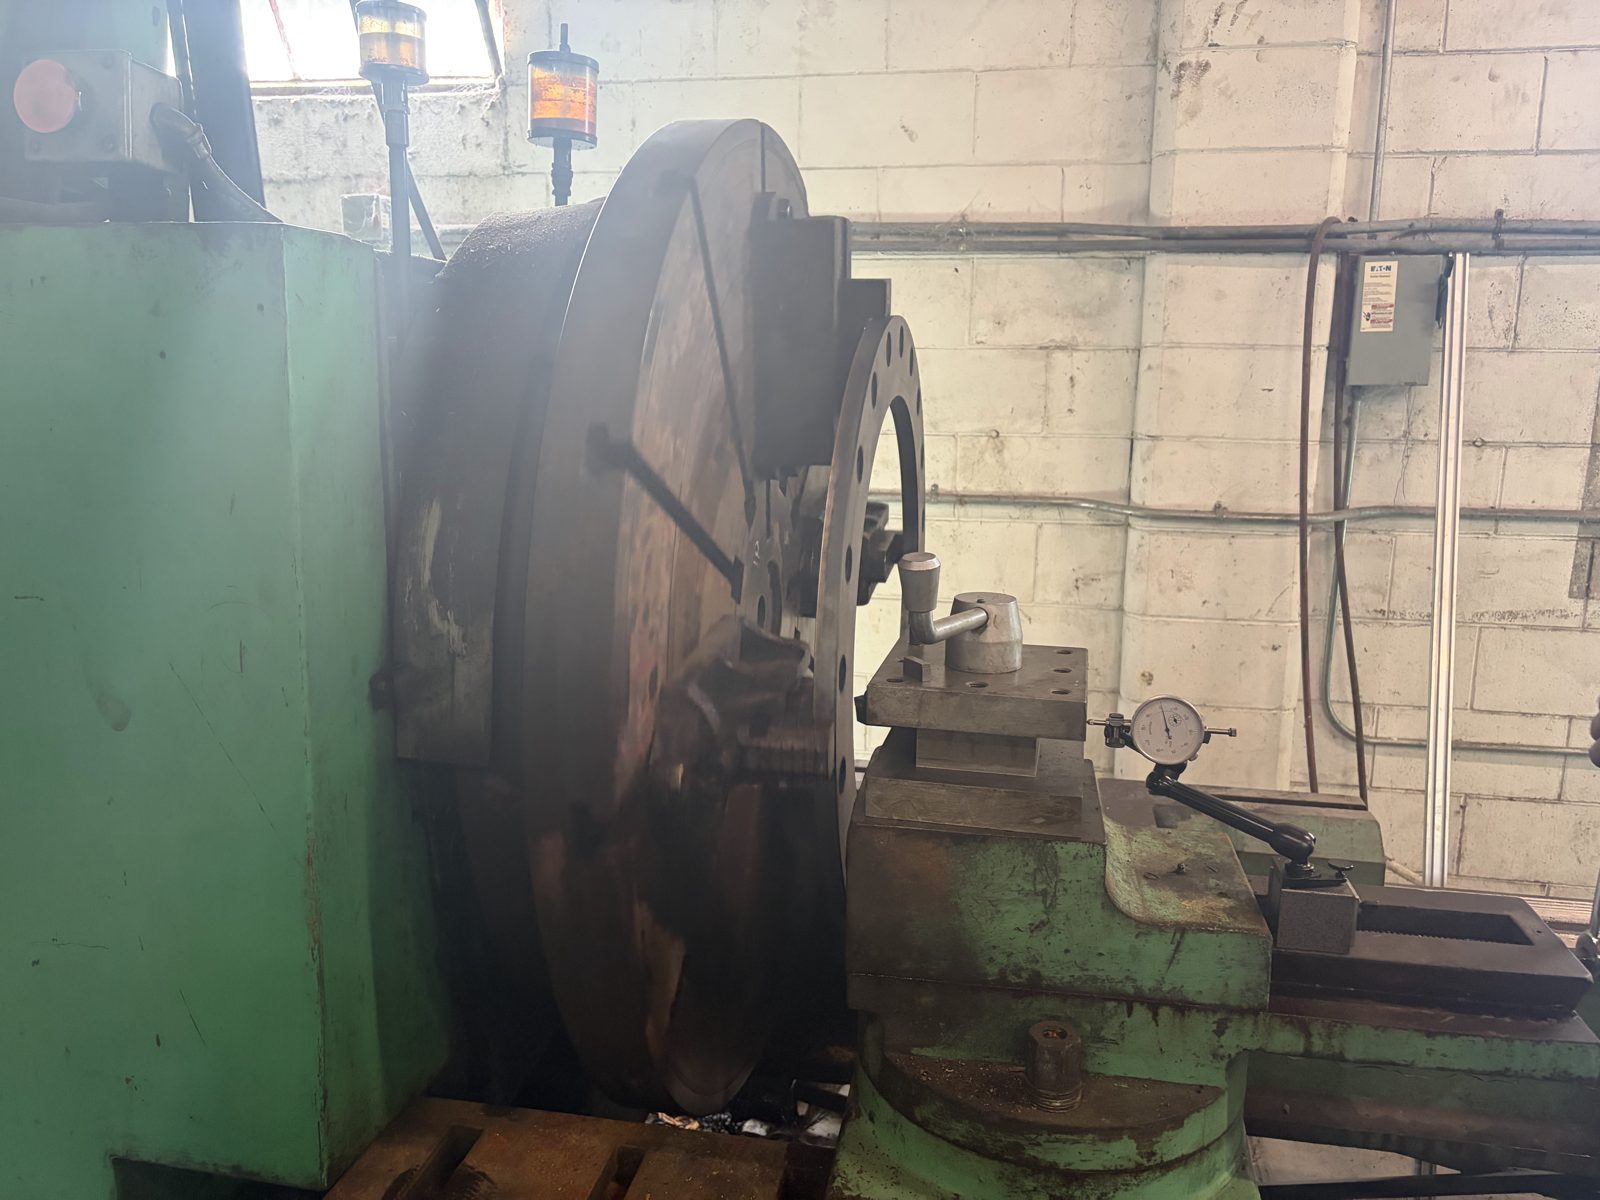
Four engine lathes, from small bushings and pins up to shafts, flanges, and cylinders most shops cannot swing: 48 inches of swing, 32 inches over the carriage, 16 feet between centers, and a through bore over 4 inches. Tolerances to ±0.001 inch.
Shafts, bushings, flanges, sleeves, cylinders, rollers, spindles, couplings, and one offs.
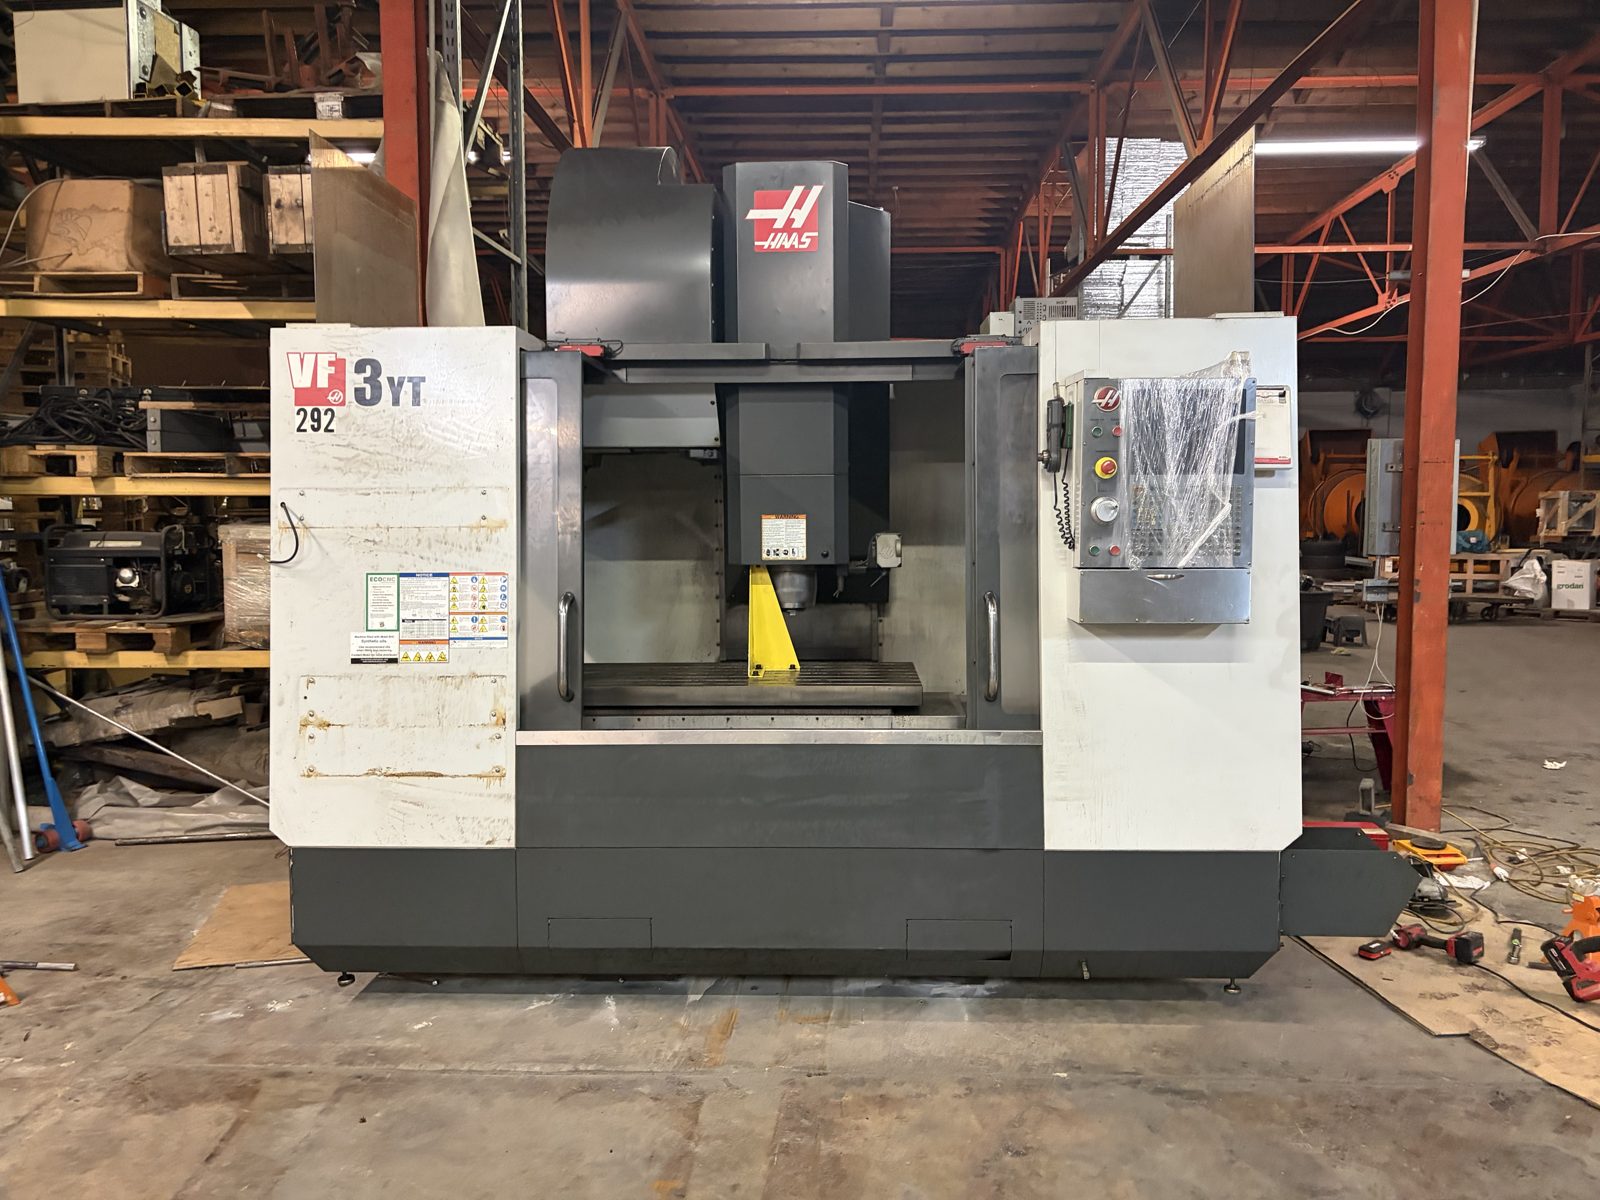
3 axis CNC milling on a Haas VF-3YT vertical machining center, 40 by 26 by 25 inch travels, 50 taper spindle, rigid tapping. The Haas takes repeat parts, hole patterns, pockets, and profiles that benefit from being programmed once and run again.
Manual knee mills with DRO handle one off repairs, keyways, counterbores, and quick fixture work in steel, stainless, aluminum, and plastics. Tolerances to ±0.001 inch.
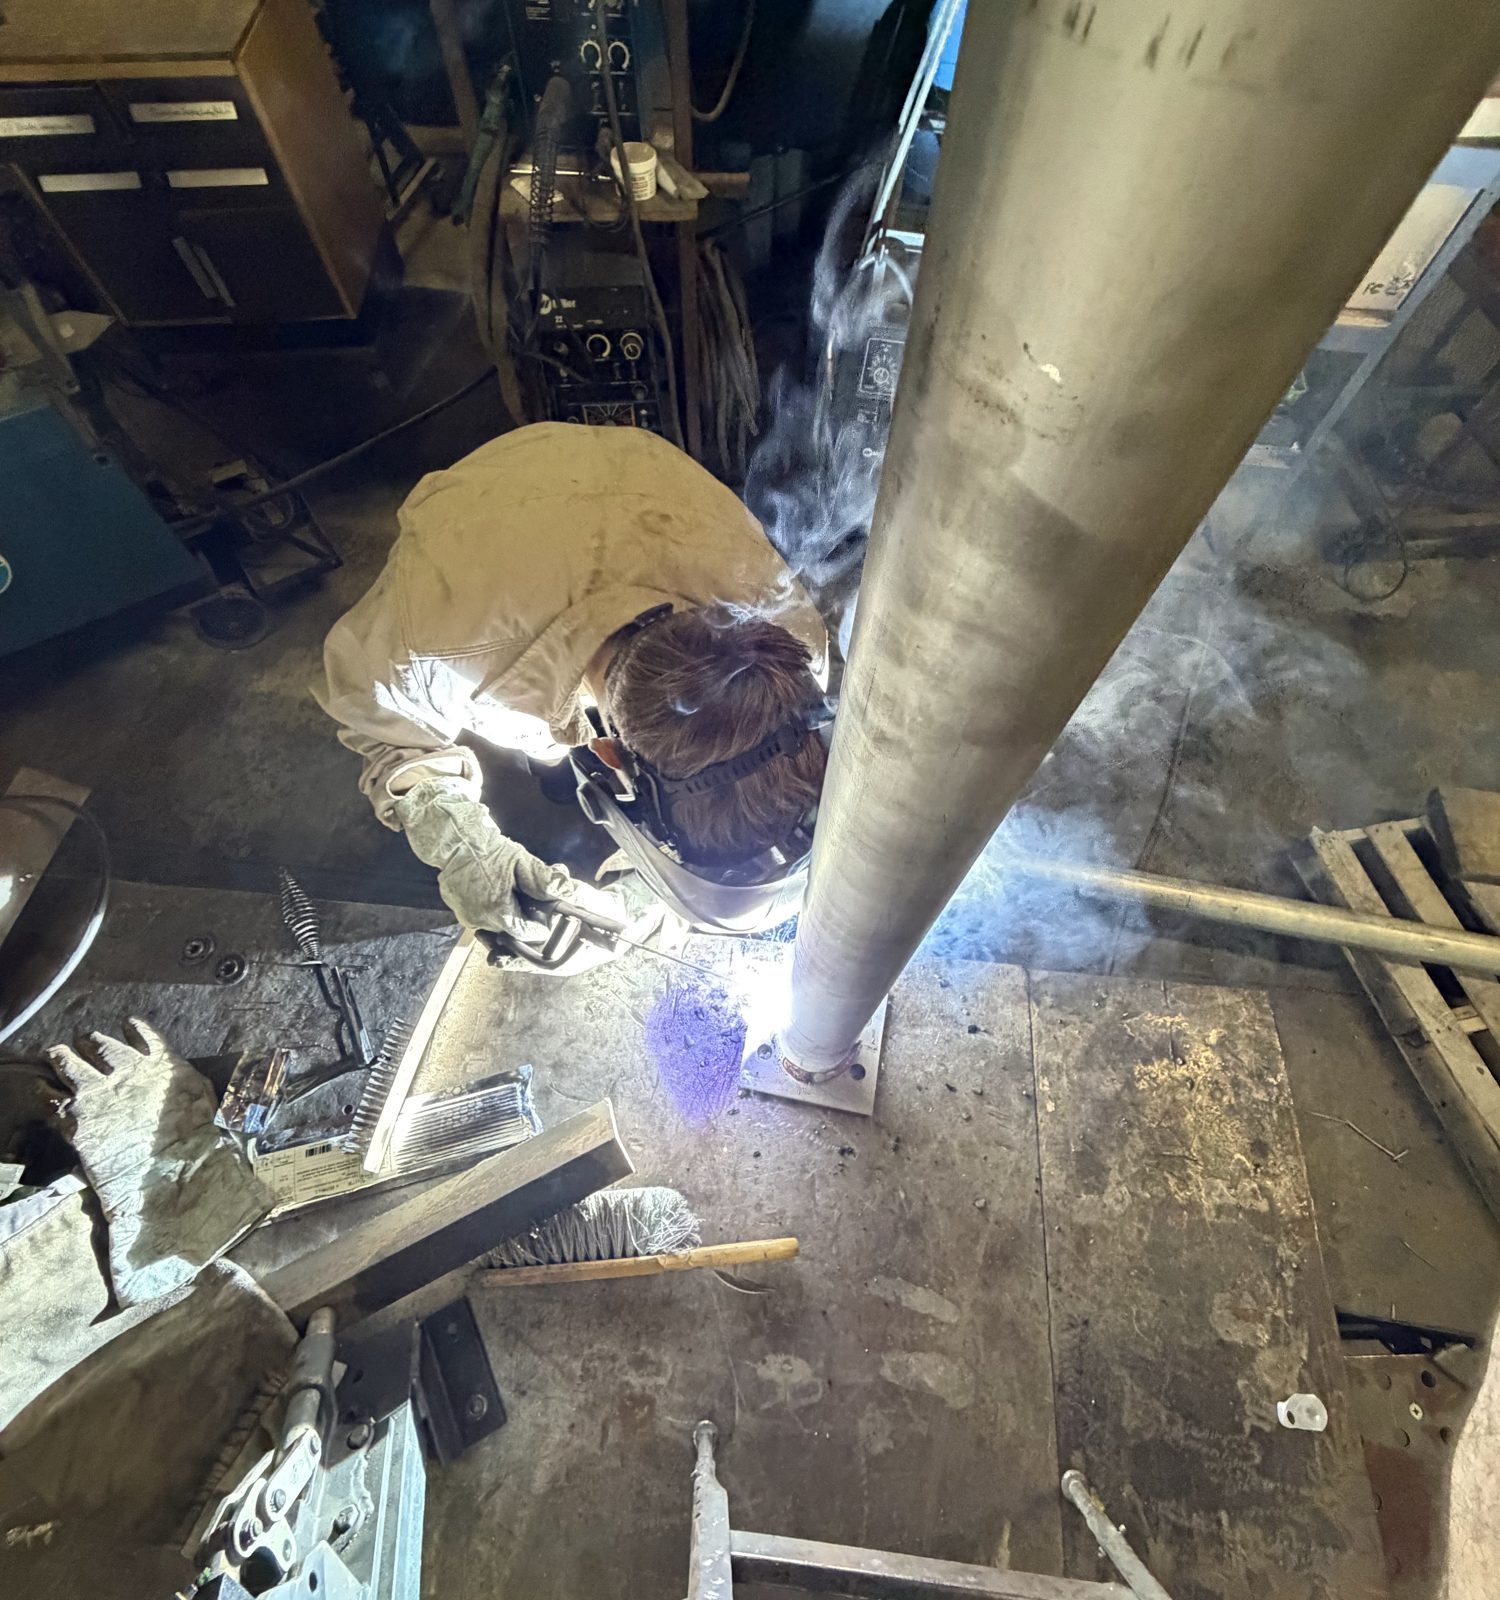
MIG (including push pull and spool gun setups), water cooled AC/DC TIG, stick, a 200 KVA spot welder, and an ABB robot for repeatable production runs. Oxyacetylene for cutting and heating.
Greg, one of the owners, is a welding engineer. For critical weldments and code work that means written procedures, procedure qualification, and process control.
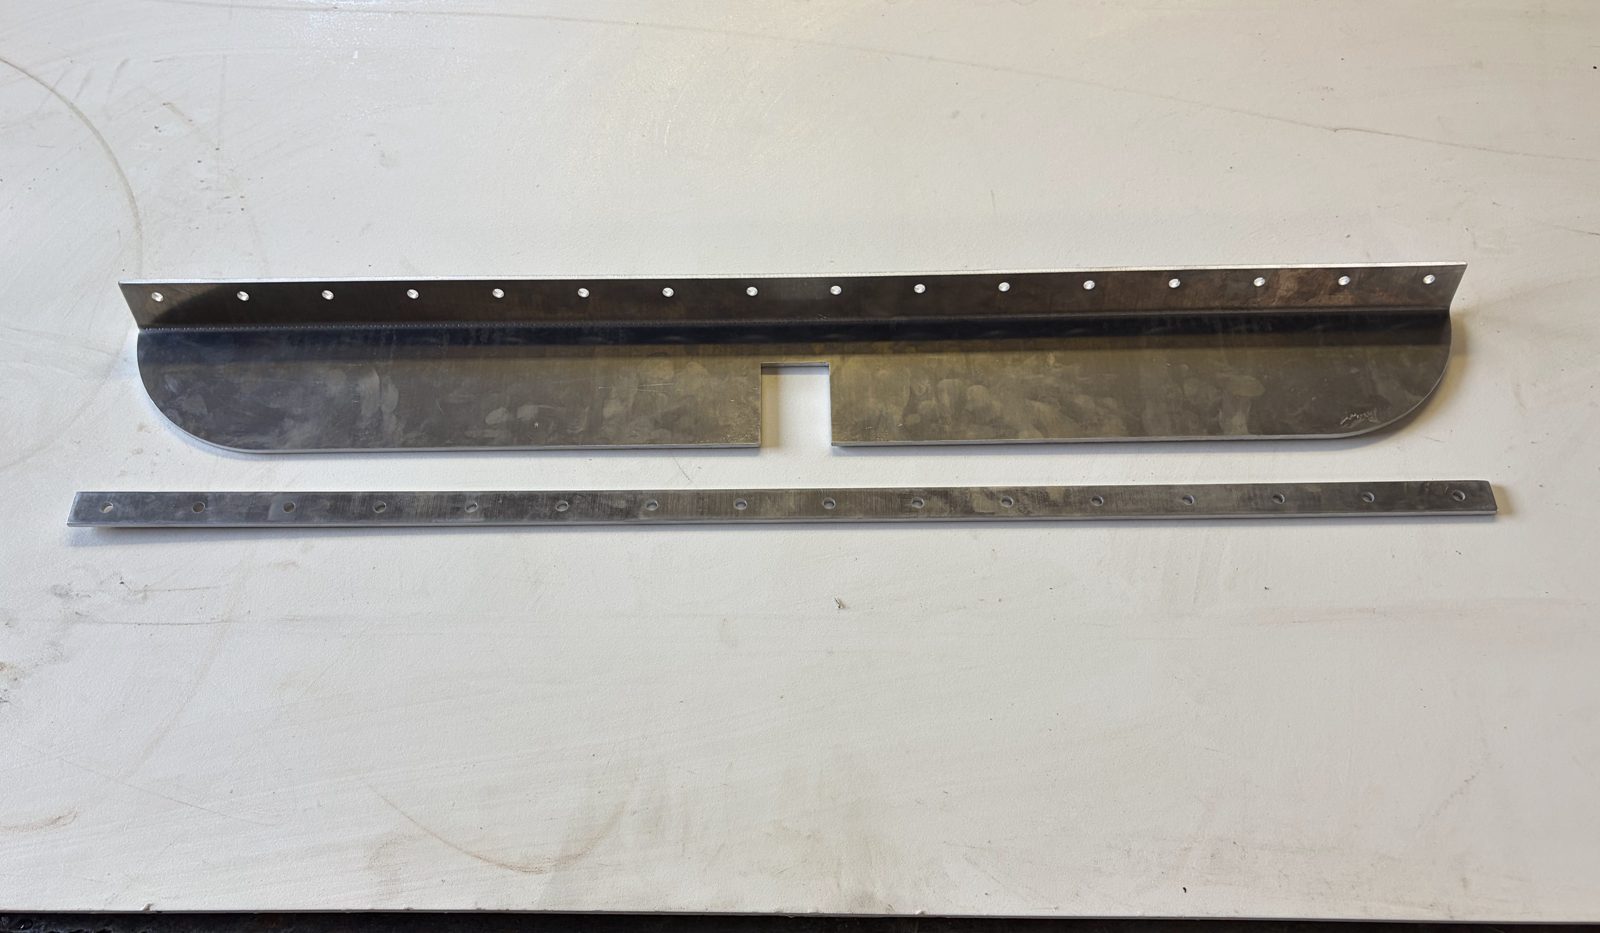
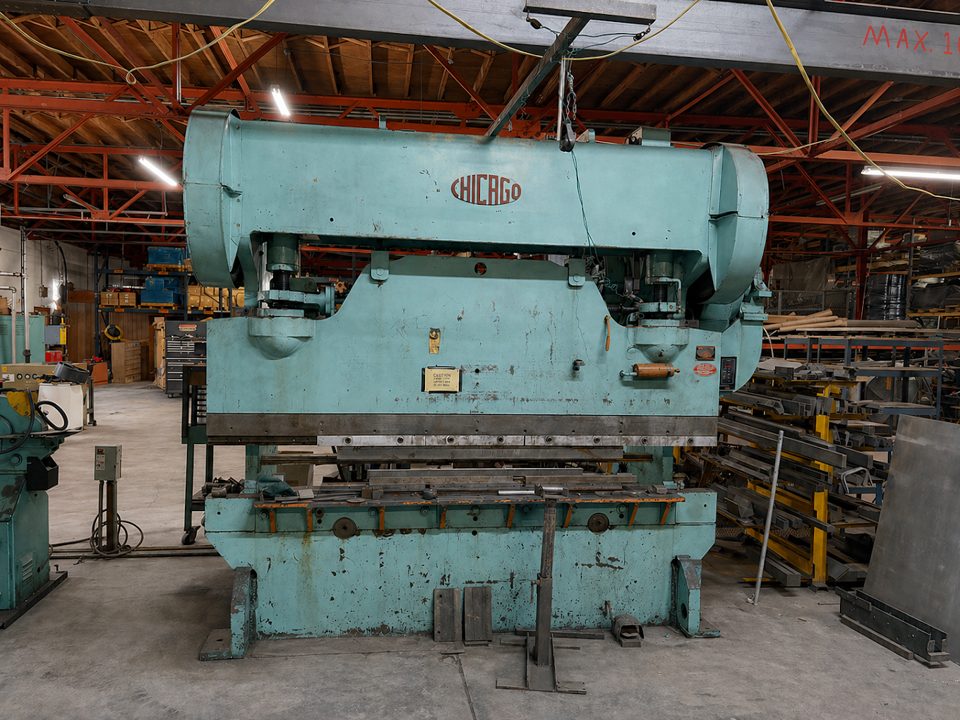
A 200 ton press brake with CNC back gauge and 8 feet of bending capacity for multi bend parts with tight angular tolerances. A 6 foot shear for plate to 1/4 inch. Laser cutting for clean profiles in sheet and plate, and CNC plasma to 3/4 inch.
A 50 ton ironworker punches, notches, copes, and shears structural shapes. 5 ton and 30 ton punch presses handle production hole work and forming.
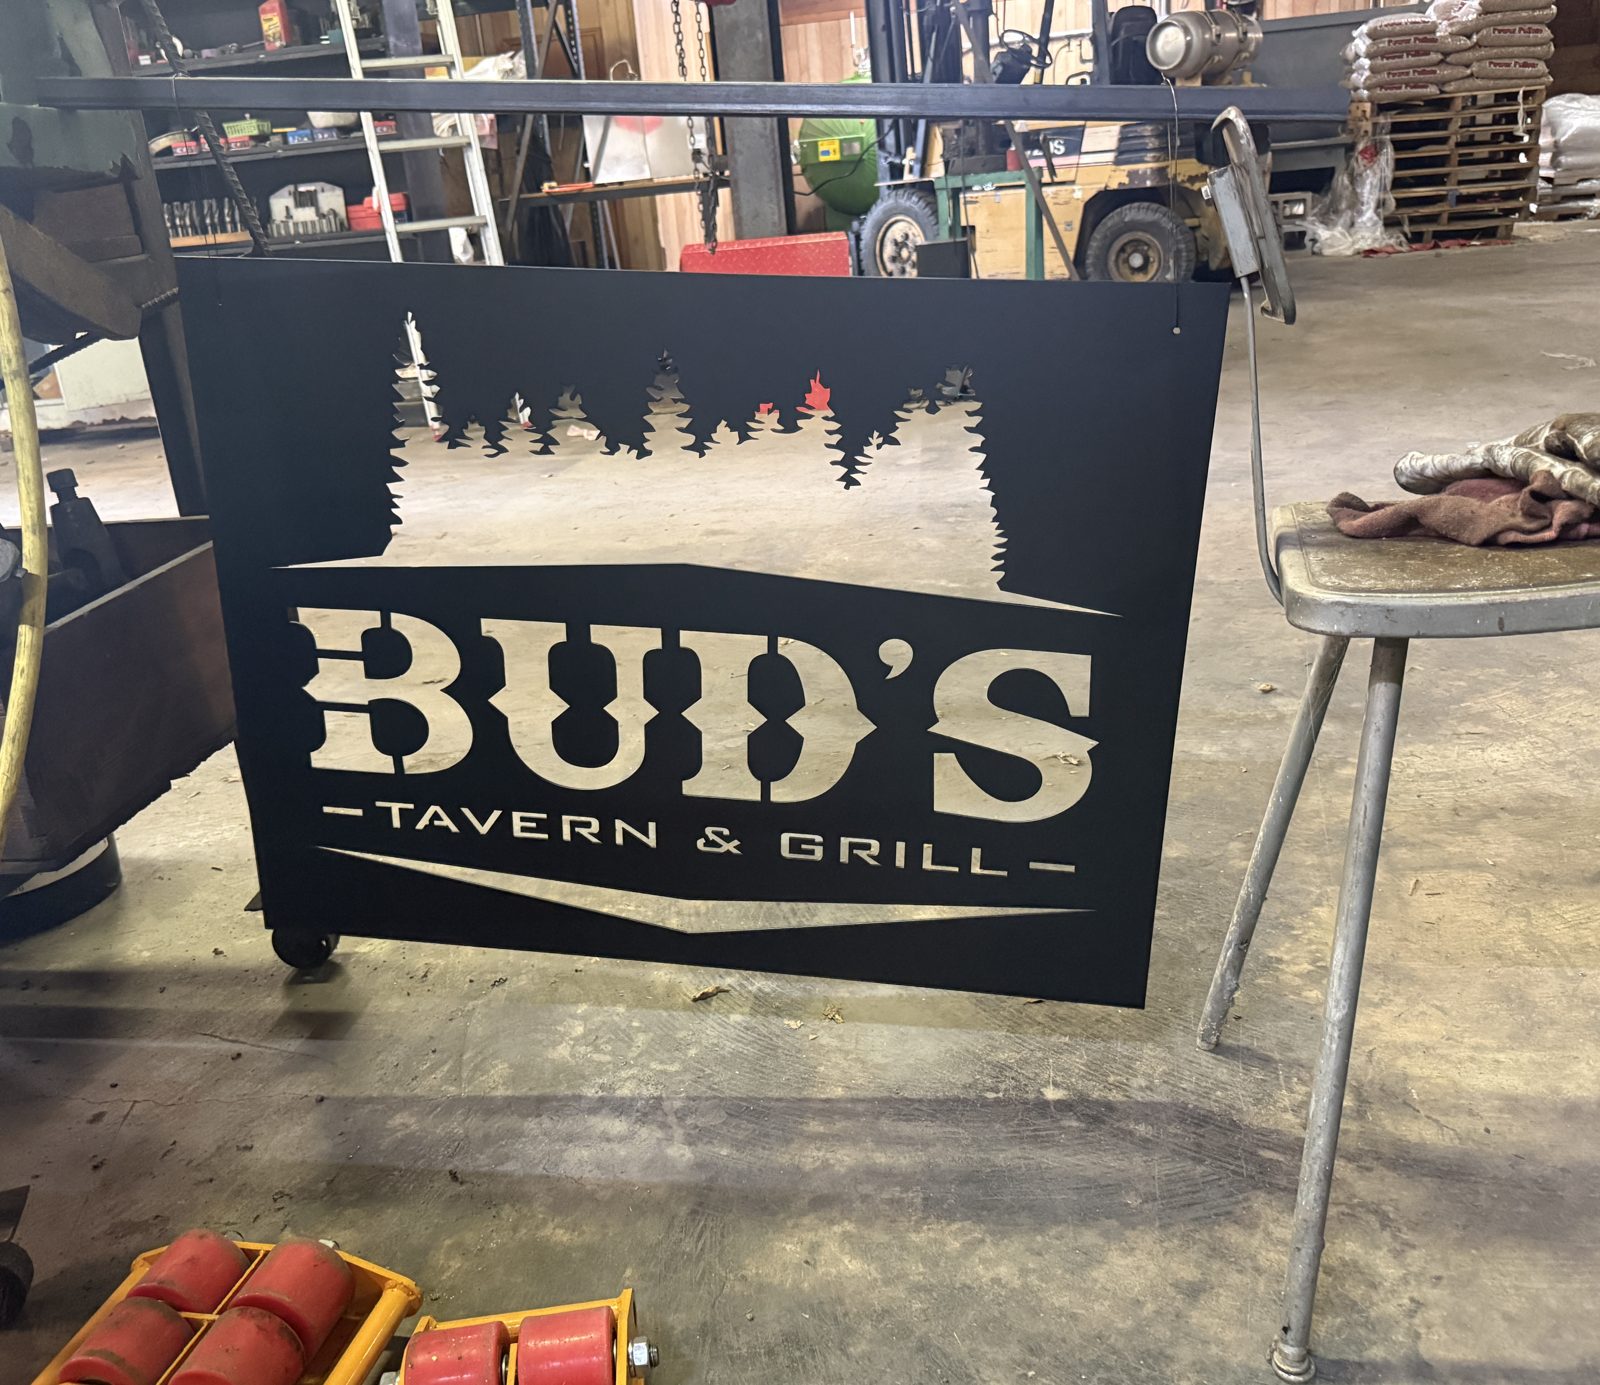
Powder coating in our own booth and a cure oven about 4 feet square and 80 inches deep, so fabricated parts get finished here instead of waiting on a coater. Surface grinding (10 by 18 inch) for flats to close tolerance. A heat treating furnace for hardening and tempering.
Sawing, drilling, tapping, reaming, deburring, pressing, and assembly. Four overhead cranes and a 10,000 lb forklift for heavy work, and an outdoor lot for staging material.
We repair and rebuild heavy equipment, make OEM replacement parts to print, and design and build custom machines from concept to installation, with operator training. Field service available.
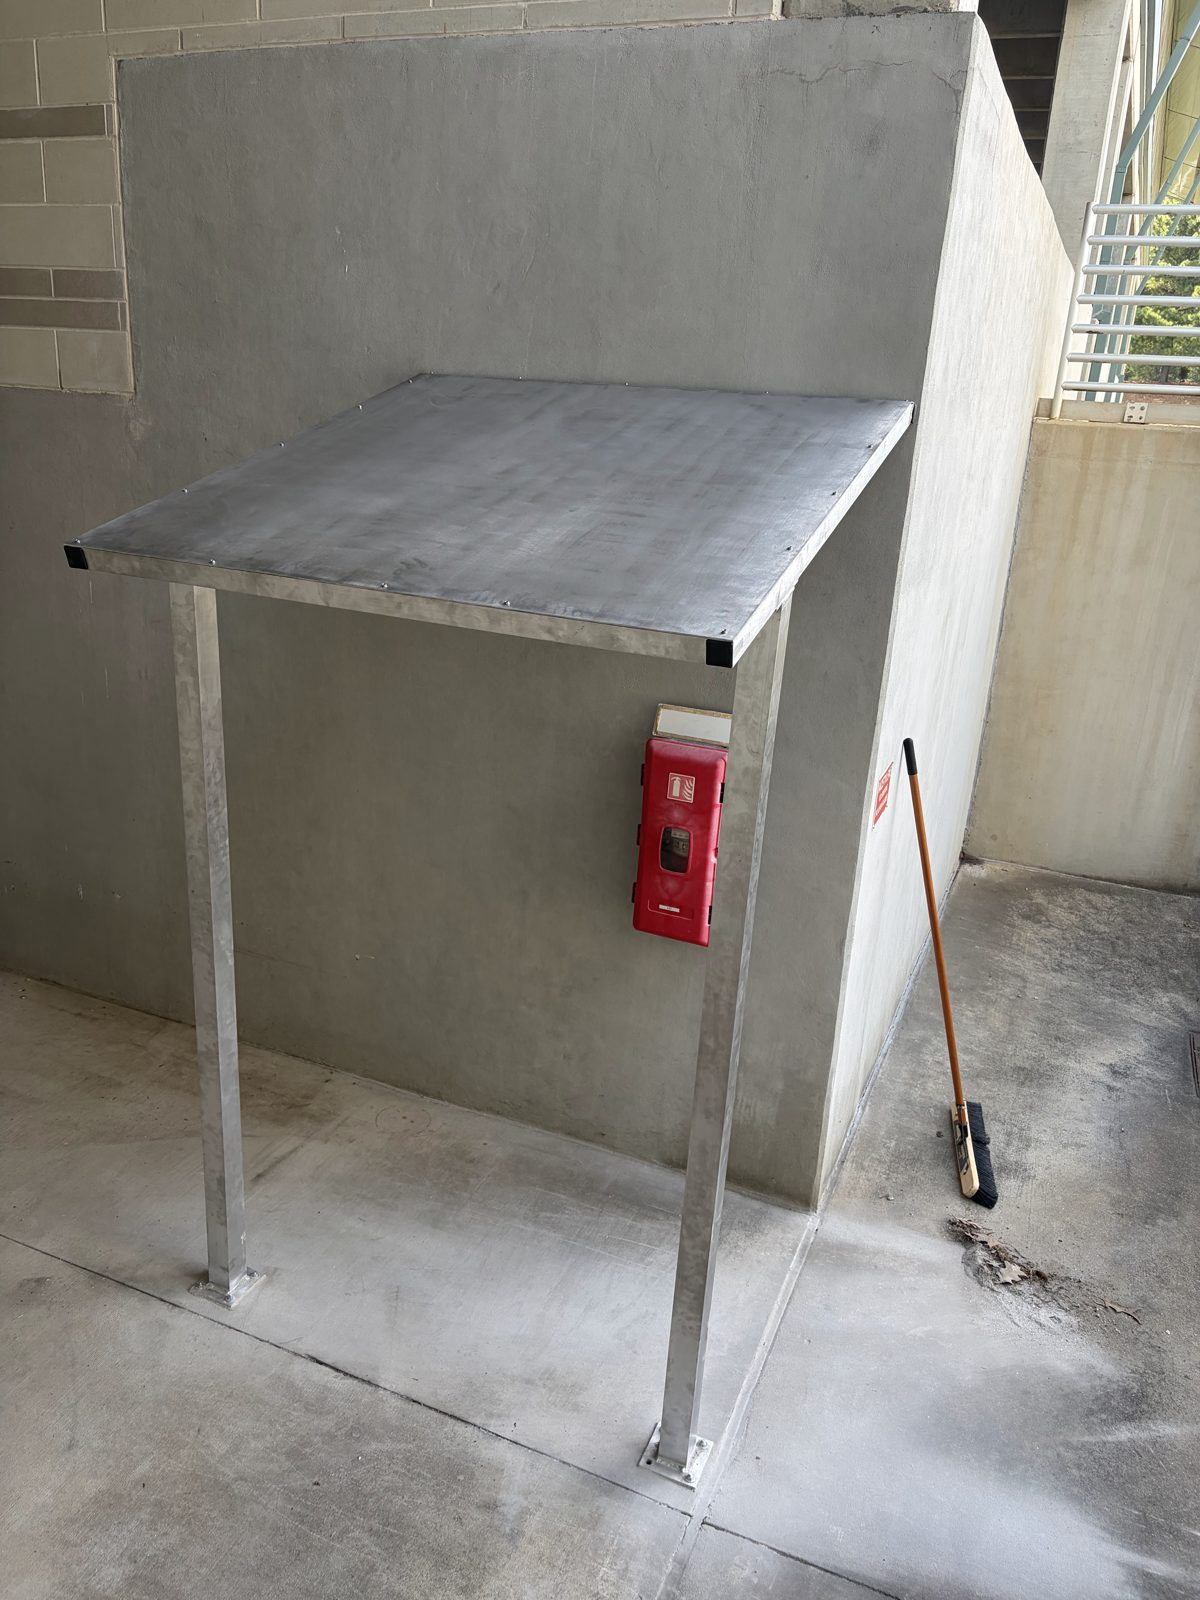
Have a part like this? Call (919) 727-6991 or send us the print. Quote and lead time within 48 hours.
